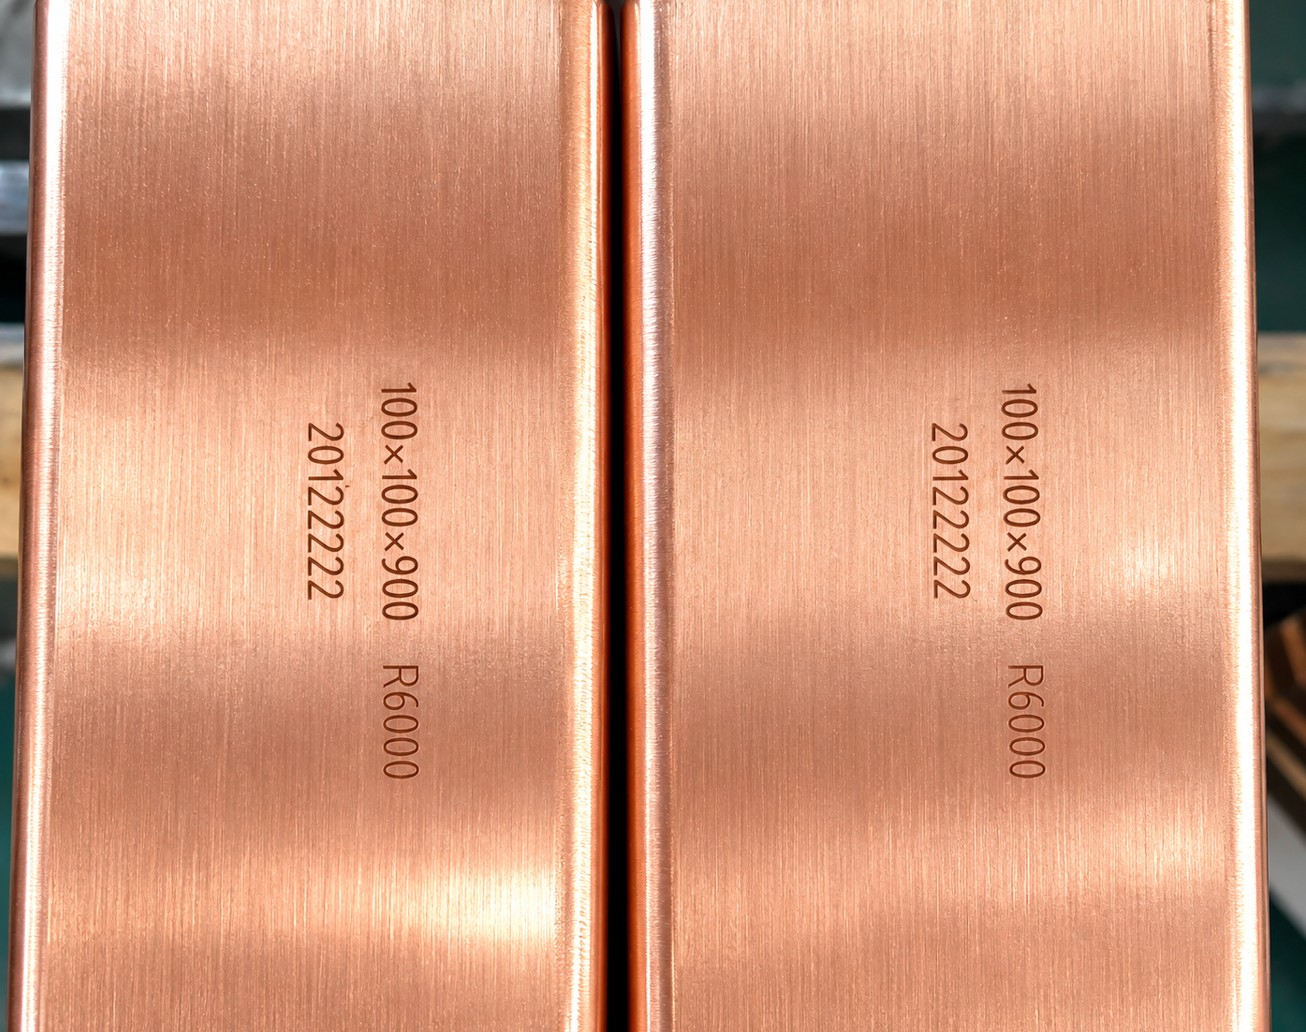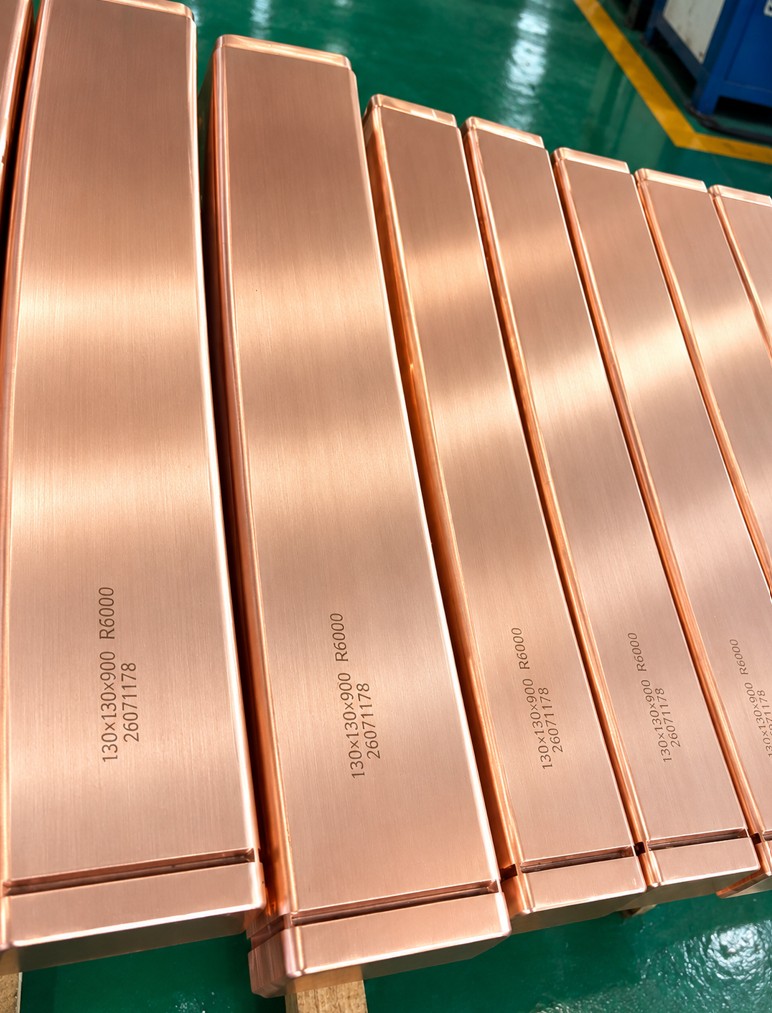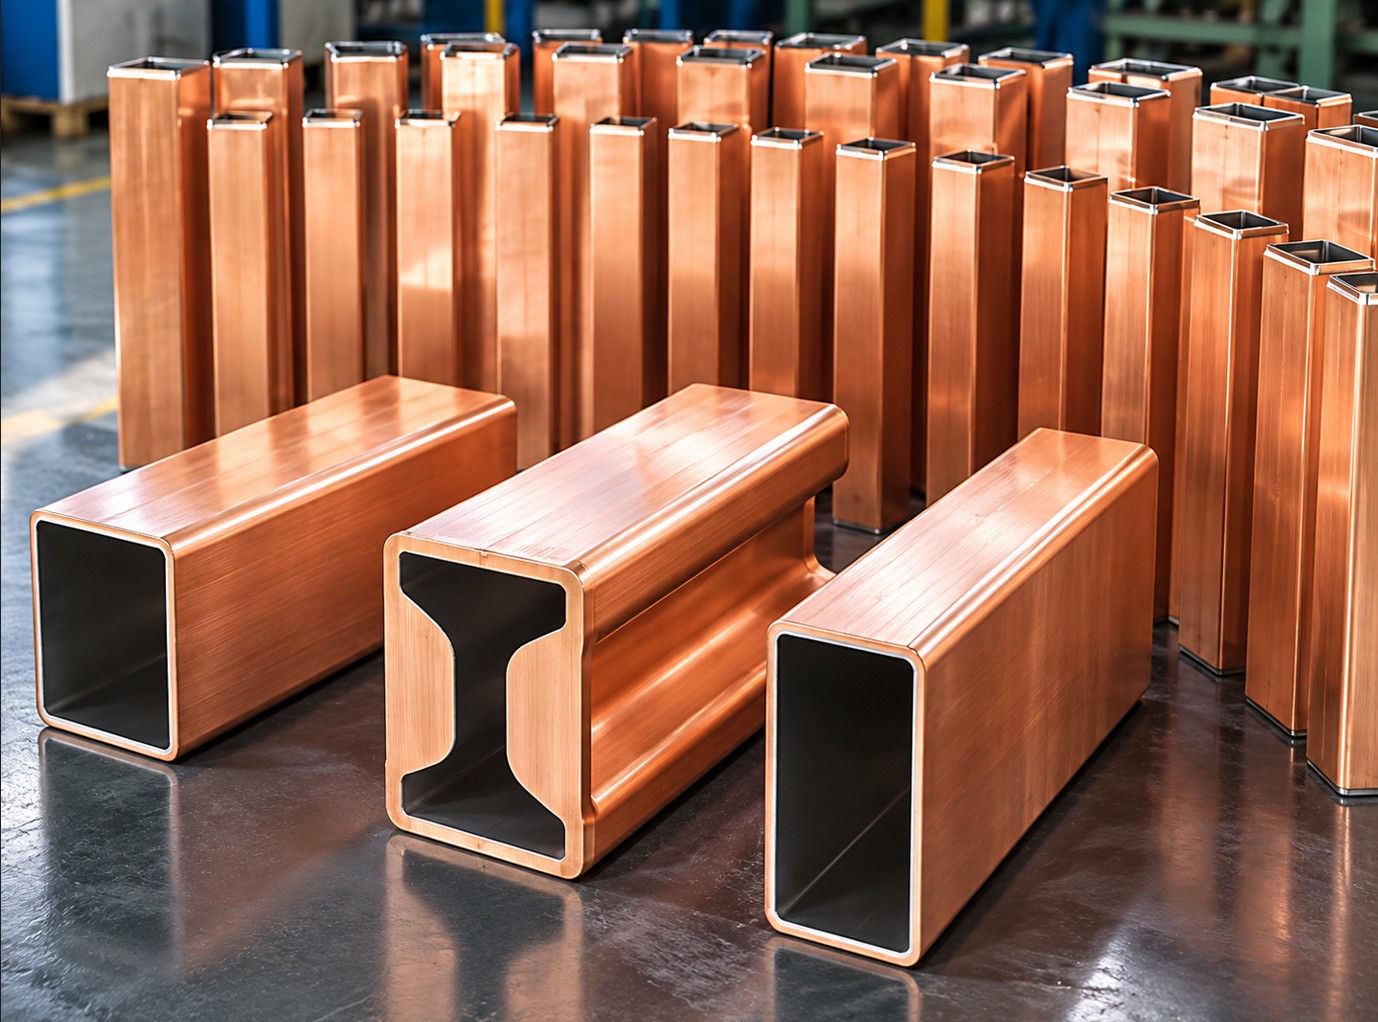
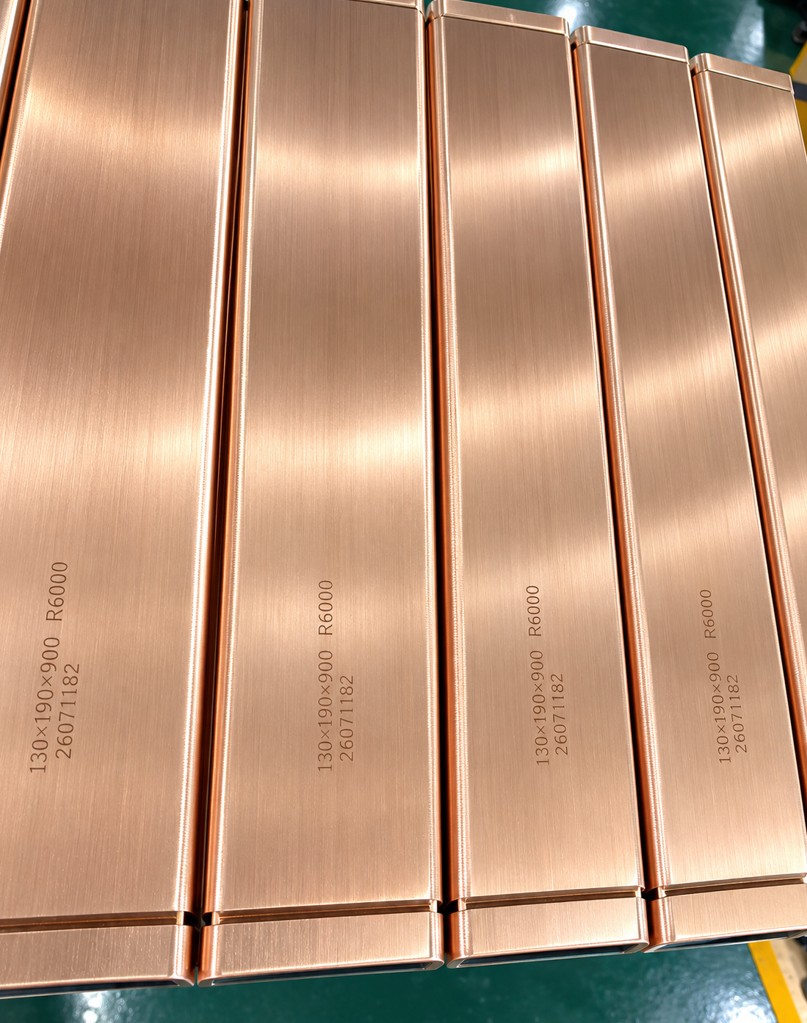
130 × 130 mm is the section most rebar and wire-rod mills cast, and R6000 is the radius most of their casters were built with. The result is that the 130 × 130 × 900 R6 tube is, with the 100 × 100, one of the two sizes we make every week. Its product page has the short specification; this article covers the decisions behind it.
| Item | Specification |
|---|---|
| Cast section | 130 × 130 mm (5.12 × 5.12 in) |
| Casting radius | R6 / 6000 mm |
| Length | 900 mm; 812 and 1000 mm on request |
| Wall thickness | 12 mm |
| Copper grade | Cu-DHP / CuAg0.1 / CuCrZr |
| Inner surface | Hard chrome 0.08–0.12 mm |
| Taper | Single / double / multi / parabolic, per drawing |
| Weight | ≈ 50 kg (12 mm wall) |
Casting speeds for 130 mm billets are typically 2.0–3.2 m/min. At the lower end, Cu-DHP gives acceptable life and is what most older casters were designed for. From about 2.6 m/min upward, or when the plant casts peritectic grades, CuAg0.1 extends taper life noticeably, and it is the grade most of our export customers now specify. CuCrZr is chosen by plants running high-speed casters or looking for maximum campaign length; at this section the price difference is easier to justify than at 100 × 100 because the tube is larger and changes cost more downtime.
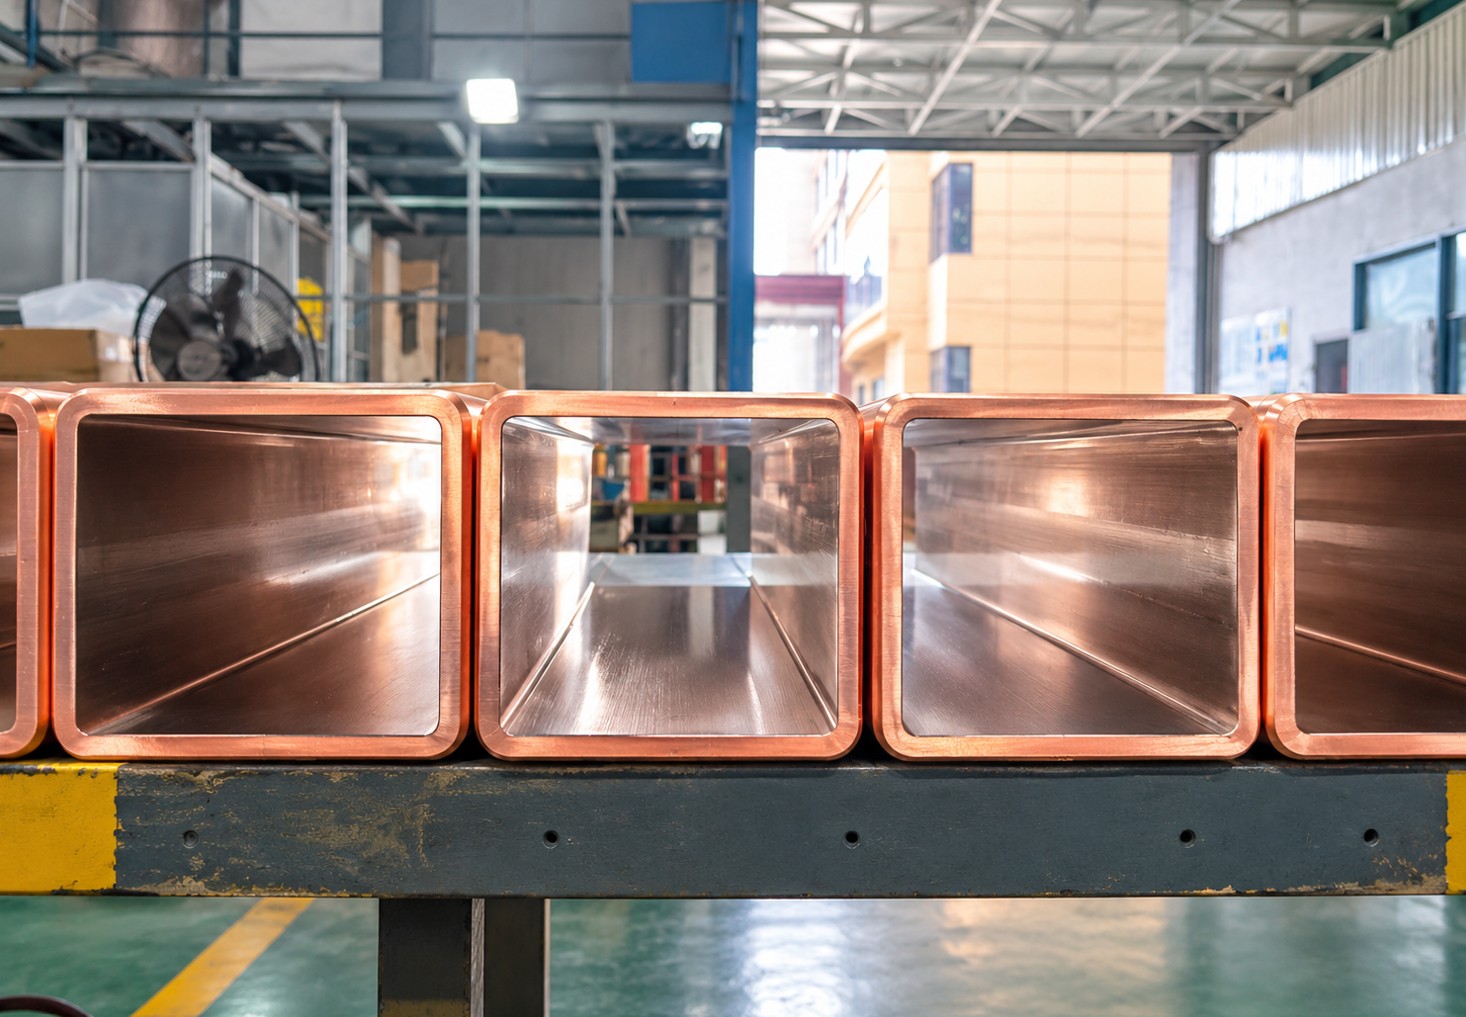
At 130 mm the corner design matters more than at 100 mm: the corners cool fastest, the shell there is thickest, and an over-tapered corner is the usual cause of off-corner cracks and rhomboidity. Most OEM designs use a corner radius of R6–R10 with a double taper. If rhomboidity is a recurring problem on your caster, send us the old tube: the wear pattern in the corners tells us whether the taper or the cooling is at fault.
Tubes for annular-gap jackets have a plain outer surface; tubes for slot-cooled jackets have longitudinal slots machined to the jacket drawing. The two are not interchangeable. If you are unsure, send a photo of the outside of the old tube, or order tube and water jacket together.
CMM report at five levels, wall and chrome thickness, mill certificate, photos before packing. VCI wrap, plywood case, four to six tubes per case. Lead time: CuAg with standard taper 2–3 weeks, other configurations 4–5 weeks after drawing approval.
Send: section confirmation, radius, length, wall, grade (or casting speed), taper drawing or OEM model, plating, quantity, port. For a first order we also ask for a photo of the old tube's marking to rule out a radius or length mismatch.
Yes: 130 × 130 × 800 R4 is a standard size, R5 and R9 to order.
1000 mm is common on newer high-speed casters; same specification, 4–5 weeks.
Yes; single tubes are quoted at the same unit price plus freight.
Related pages: 130 × 130 × 900 R6 product page · R6 Copper Mould Tube · R4 130 × 130 × 800 · Mould water jacket · Specification tables