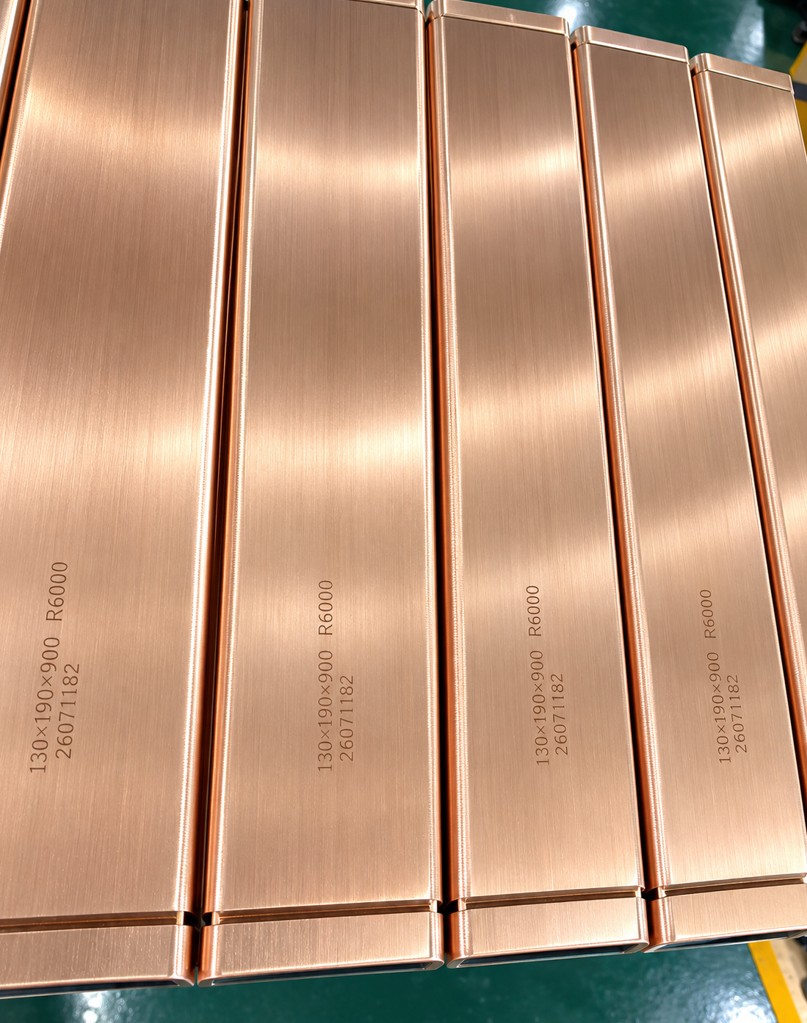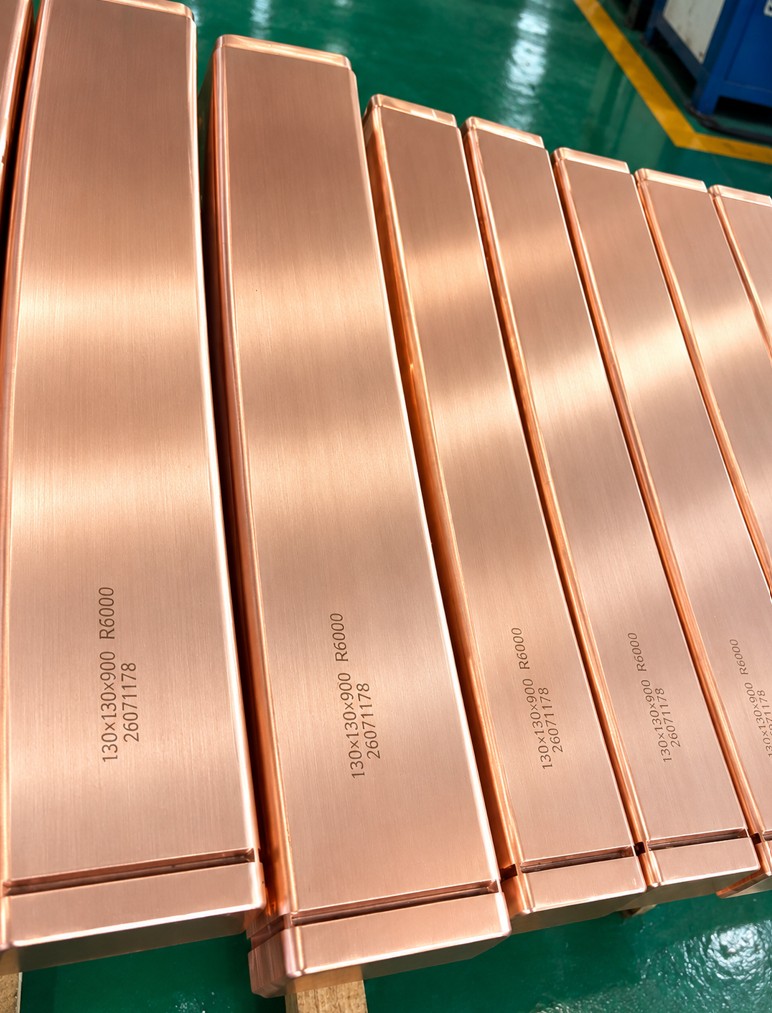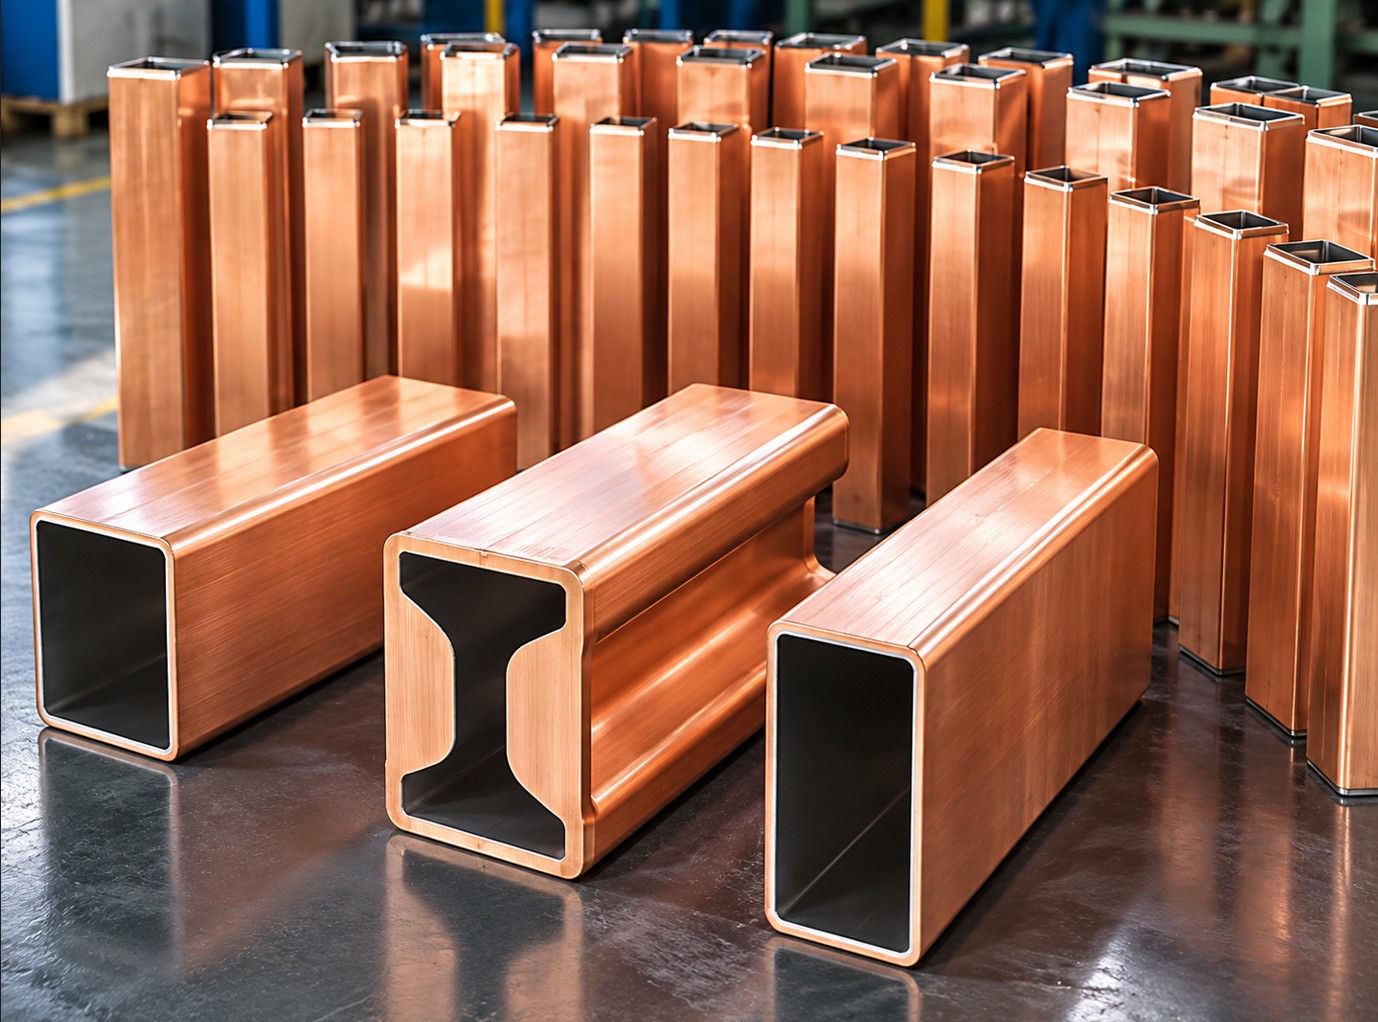
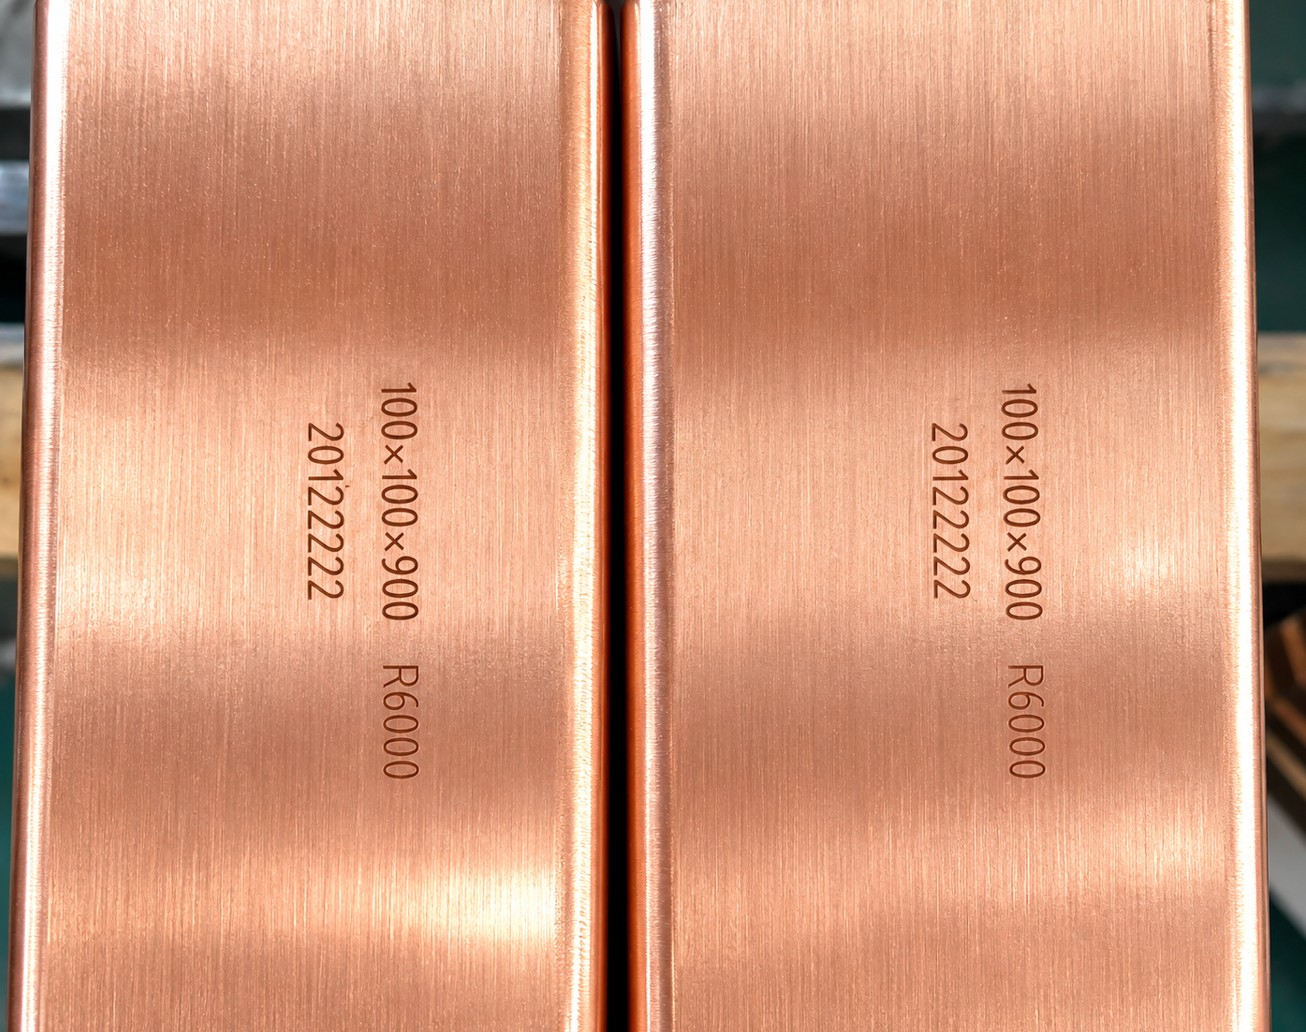
If a steel plant casts 100 mm square billets on an R6000 machine, this is its tube. We produce it continuously and hold it in stock in CuAg, which is why it has its own product page. This article is the long version of that page for buyers who want every detail before ordering.
| Item | Specification |
|---|---|
| Cast section | 100 × 100 mm (3.94 × 3.94 in) |
| Casting radius | R6000 mm (236.2 in) |
| Length | 900 mm (35.4 in); 812 and 1000 mm on request |
| Wall thickness | 12 mm standard; 10 mm optional |
| Copper grade | TP2 / Cu-DHP, CuAg0.1 or CuCrZr |
| Inner surface | Hard chrome 0.08–0.12 mm; Ni-Cr optional |
| Taper | Single, double, multi or parabolic, per OEM drawing |
| Corner radius | R4–R8 mm typical, per drawing |
| Water cooling | Plain outer surface for annular gap, or machined slots per jacket |
| Weight | ≈ 37 kg (CuAg, 12 mm wall) |
At 100 × 100 the section is small, the shell forms quickly, and casting speeds are high: 3–4.5 m/min is normal on modern casters. That puts the meniscus copper temperature into the range where Cu-DHP softens, so CuAg0.1 is our default recommendation and the grade we stock. Cu-DHP remains a valid choice for older casters running under 2.5 m/min. CuCrZr is rarely needed at this section unless the plant is running above 4.5 m/min or casting very hot grades.
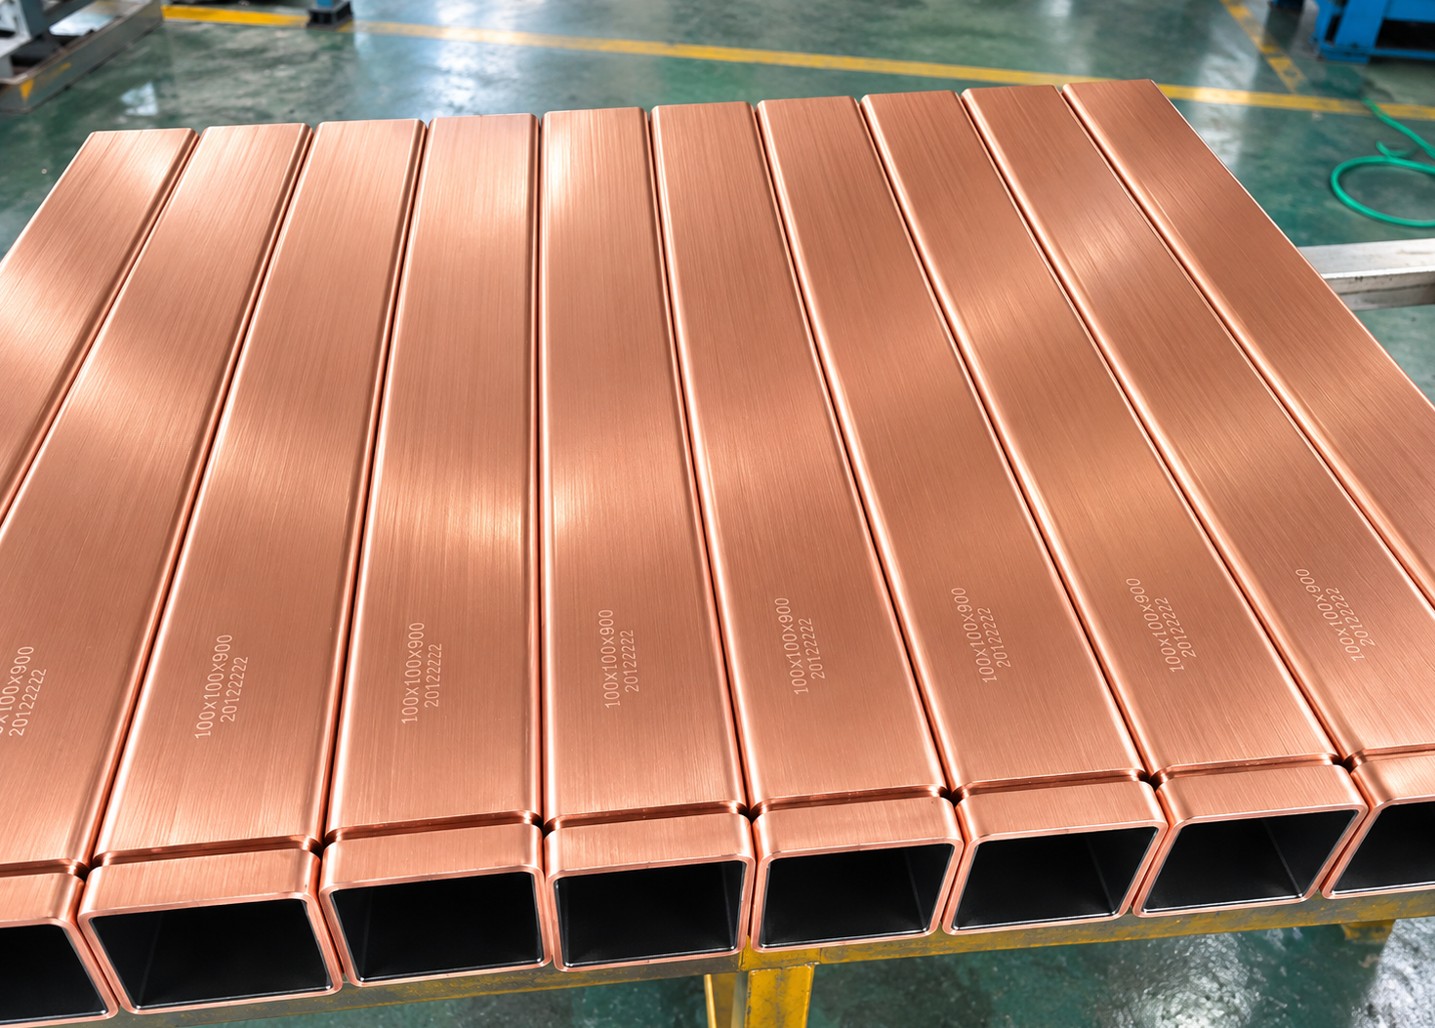
Because of the high speed, most 100 × 100 casters use a double or parabolic taper with a steep upper segment. If your caster is from a known OEM, tell us the model; we have taper data for the common designs. Otherwise send the old tube drawing, or give us the casting speed and we propose a profile.
Every tube ships with a CMM report (section at five levels, taper, radius, length), wall thickness at eight points, chrome thickness at six points, surface roughness and the copper mill certificate. Photos are taken before packing. Tubes are wrapped in VCI film, boxed individually in plywood cases with foam supports, 4–8 tubes per case depending on your order.
CuAg 12 mm wall with our standard double taper: from stock or 2–3 weeks. Other grades, tapers or slot patterns: 4–5 weeks after drawing approval. Air freight is practical for urgent orders; a case of four tubes weighs about 170 kg.
CuAg, 12 mm wall, standard double taper: usually yes. Ask for current stock.
812 mm (32 in) is common on older casters; same price, 3–4 weeks.
Yes; we manufacture to the drawing and the CMM report is against the drawing dimensions.
Related pages: 100 × 100 × 900 R6 product page · R6 Copper Mould Tube · 130 × 130 × 900 R6 · Copper materials · Specification tables